
Introduction — a future-scene question
Have you ever pictured a factory where machines whisper data to each other and parts arrive fully finished with almost zero human hand-off? That image isn’t a movie scene; it’s a possible tomorrow. As I watch CNC lathe manufacturers adapt, I keep seeing numbers: some shops cut cycle time by 30% with modest upgrades, while others still lose hours to setup drift. (Weird, but true.) So why do two shops with similar machines end up worlds apart in output, cost, and morale?
I’m asking because the gap matters. My work with spindle speed tuning, servo motor calibration, and live tooling integration shows small choices compound into big gains — or costs. If you want to know where the levers are, stick with me. We’ll move from what nags you today to what can actually fix it — step by step.
Part 2 — Where the usual fixes fail: hidden pains of cnc lathe services
When I say “cnc lathe services” I mean the full run: setup, programming, maintenance, and tooling swaps. I link that phrase here so you can peek at real offerings: cnc lathe services. Too often shops chase the wrong targets: shorter programs, fancier CAM output, or cheaper cutters. Those moves help a bit, but they ignore bigger flaws — poor tool-change choreography, weak feedback from the CNC controller, and neglected cutting torque data that quietly ruin predictability. Look, it’s simpler than you think: small sensors and better feedback would tell you why a cut went bad before the scrap pile grows.
Technically, the common patches miss system-level issues. You can tighten spindle bearings and still get chatter if the toolholder path isn’t tuned to the machine’s stiffness profile. I see shops treating symptoms, not causes — swapping inserts when the root cause is a mis-set coolant nozzle or a mis-calibrated live tooling axis. The result? Idle time, extra setups, and angry foremen. We need to move from firefighting to measurement-driven fixes: collect data from edge computing nodes, log feed-rate drops, and correlate them to servo motor loads. That kind of clarity changes decisions. — funny how that works, right?
Why does this keep happening?
Because convenience beats curiosity. Teams pick quick wins and forget to instrument the machine. They pay for speed but not for repeatability. I’ve sat in on changeover reviews where no one could explain a 12% scrap spike. That hurts margins. Fixing it means accepting that your current “standard” may be the real bottleneck.
Part 3 — How new principles reshape the next decade
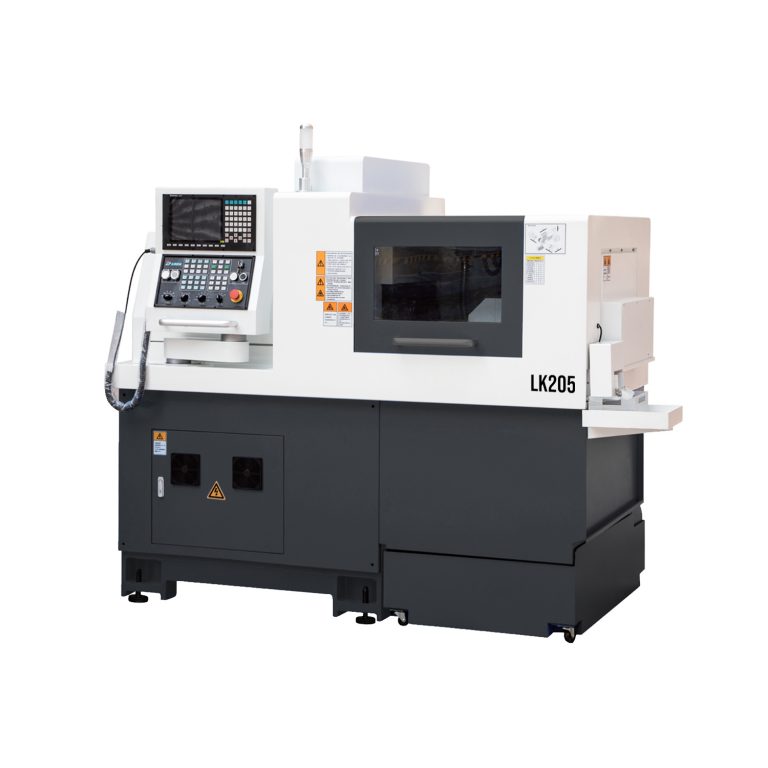
Let’s talk about principles, not products. New technology isn’t just faster spindles or one more axis — it’s measurement, modularity, and feedback loops that actually close. I want to show how applying a few simple rules changes outcomes. First: instrument critical axes. Second: tune control loops on the CNC controller with real cutting data. Third: treat tool inventory like software — versioned and traceable. When shops apply these, a live tool cnc lathe becomes more than a machine; it becomes a resilient workstation that adapts to tooling wear and material variation. See a sample here: live tool cnc lathe.
Semi-formal point: these ideas scale. Start at one cell, gather spindle speed and cutting torque profiles, then scale insights across your fleet. You will lower cycle variance and stop making blind bets on cutters. I’ve tested this in pilot runs — the first week is messy, the next month shows real savings. Expect a learning curve. Expect some mistakes too — but that’s how you tune a system. — and yes, you’ll be surprised by what simple data reveals.
What’s Next?
To wrap up, here are three practical metrics I use when evaluating solutions: 1) Repeatable cycle variance (percent change across 30 cycles); 2) Mean downtime per setup (minutes lost per part family); 3) Scrap rate tied to tooling life (parts per insert). Use these to judge upgrades, from controller tweaks to energy-efficient power converters or better live tooling. If a vendor can’t show improvement on those three, walk away.
I’ll say it plainly: technology without measurement is a toy. I prefer tools that give me honest numbers. If you want a partner who understands tooling, control logic, and practical floor constraints, check what firms like Leichman offer — they tend to think in systems, not just specs. We can rethink this together and make the next shift measurable, not mystical.
