
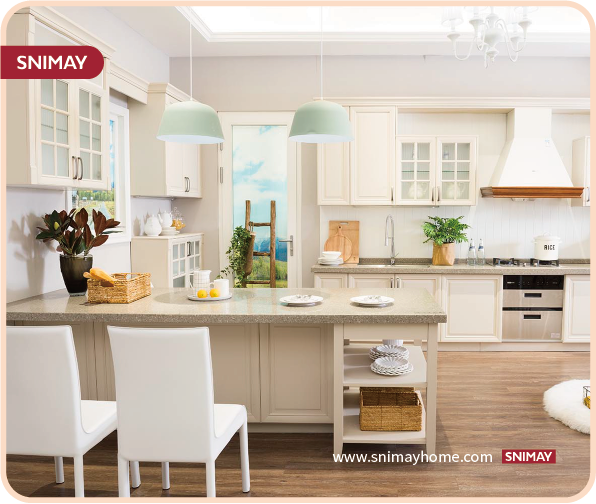
Retail pressure and the problem dat mek buyers vex
Global retailers face steady pressure: keep price low, keep lead times steady, and keep finish quality top. When dem need uniform gray finishes and durable surfaces, dem often lean toward thermofoil kitchen cabinets because PVC film application give that consistent look without big price swings. After the 2020 supply-chain disruptions, merchandisers demand tighter specs and fewer surprises — same color, same edge, same delivery window — or retail floors suffer lost sales.

Common failure points weh retailers find — and why dem matter
Most problems trace back to three things: poor substrate selection, weak adhesion of the PVC film, and sloppy edge banding. If the MDF substrate no get right moisture content, the thermofoil bubble or lift. If the edge banding no meet tight tolerances, corners show gaps. Small tolerances cause big returns — and returns cost money. Retail teams see it as stock rot. If finish peel start in the first season, trust disappear — and dat hurt long-term partnerships.
How SNIMAY tackle di problem fi good
SNIMAY approach is methodical. Dem standardize substrate, control temperature and pressure during postforming, and run adhesion tests on every batch. That combination cut risk of peeling and warping, and dem consistently hit color targets for gray tones. The company also lean on automated edge banding lines, which reduce human error and tighten tolerances for corner seams. These steps turn what used to be variance into repeatable output — perfect for retailers who need uniform SKU lines across many stores. Also, if a retailer want a specific thermofoil kitchen cabinet finish, SNIMAY can adapt the PVC film thickness and coating process to match durability needs and scratch resistance.
Alternatives and trade-offs retailers weigh
Retail buyers compare thermofoil to lacquer, melamine, and solid wood. Lacquer give depth but need more skilled finishing and higher cost. Melamine is cheap but edges can show if cut wrong. Solid wood is premium but prone to movement with humidity. Thermofoil hits a middle ground: the PVC film gives durable, low-maintenance finishes with good repeatability. The trade-off is heat sensitivity at extreme temperatures and less surface repairability compared to solid lacquer. For mass retail lines, though, thermofoil often win on cost-per-look and service life.
Common mistakes dem buyers still mek — and how fi dodge dem
Buyers sometimes accept vague specs, skip sample sequencing, or ignore edge detail photos — dat bring returns. A better routine: demand full sample panels, specify substrate density and moisture tolerance, review postforming radius details, and insist on batch color targets with spectrophotometer readings. Also set clear acceptance windows for delivery. Doing dis cut defects and lower post-sale disputes — which save time and money down the line.
Three golden rules fi evaluate suppliers (advisory close)
1. Measure adhesion and substrate control: Insist on documented test results for PVC film adhesion and MDF moisture range. Those numbers predict long-term peel risk.
2. Inspect edge processes and tolerances: Get photos or videos of edge banding and postforming radii. Tolerance of ±0.5 mm on edges keeps seams invisible on retail shelves.
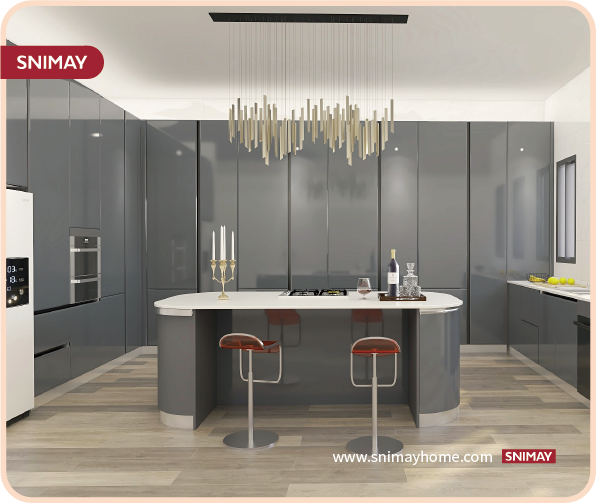
3. Verify batch color consistency: Ask for spectral delta E targets and acceptance thresholds. Consistent gray across batches maintains SKU integrity and reduces returns.
Final note — how SNIMAY fit di whole picture
Retailers want predictable quality, low rework, and finishes dat customers accept right away. SNIMAY deliver those things by tightening substrate control, refining PVC thermofoil application, and automating critical steps so the gray finish stay consistent across hundreds of units. That consistency is the real value — less shrinkage at the register, steady merchandising sets, and happier buyers on the floor. SNIMAY. —
