
Where molded bottles go wrong (and what I saw on the line)
I remember the morning of March 12, 2019 at our Ho Chi Minh City fill-finish line: a supervisor shouted about stuck stoppers while we watched batches backing up — that scene stuck with me. The second sentence here must say it straight: a pharma glass bottle that looks fine can hide microscopic stress points that break sterility downstream. Early in that shift we found the culprit in our molded bottles run — thin neck radii on a Type I borosilicate 10 ml vial causing 14% micro-crack rejects (12,400 units wasted); how can anyone justify those losses? I’ve handled B2B sourcing for over 15 years, buying amber glass, setting capping specs and tracking sterility failures — and honestly, no kidding, the common fixes we tried first barely moved the needle (trust me).

What was the hidden pain?
The deeper layer here isn’t just breakage; it’s the silent costs. We lost lead time, paid expedited freight, and endured a 6-week client audit in April 2019 — that single molded bottles run cost us near 8% of the project margin. The flaw wasn’t visible in a basic visual inspection: it was tooling tolerance, polymer residue from incorrect oven profiles, and inconsistent annealing schedules that shifted the internal stresses. I firmly believe the traditional approach — buy the cheapest vial from a catalog, hope for the best — is flawed for regulated products. Sterility and compatibility (extractables, leachables) matter; so do supplier traceability and batch-level testing. This is where many procurement teams hit the wall.
Comparative fixes and a technical roadmap
I want to shift speed now and be forward-looking: compare what we did versus what worked for several clients last year. Technically, you must treat molded bottles as a system: mold design, blank annealing, surface treatment, fill-finish compatibility and tamper-evident capping all interact. In 2021 I recommended moving from generic soda-lime runs to a strict Type I borosilicate spec for a vaccine component—production variability dropped from 9% to 1.8% within three months after we standardized tooling and adjusted the annealing curve. That improvement came from measurement — not hope. If you’re comparing suppliers, look beyond price: request process capability (Cp/Cpk), insist on documented sterilization cycles, and require representative extractables data. I’ll say it plainly: testing matters. We documented each change and saw measurable ROI—so yes, this is doable.
What’s Next?
Moving forward I compare options using concrete metrics — that’s my short checklist. First, supplier process capability: demand Cp and Cpk for dimensional tolerance and breakage rate. Second, material certification and sterility validation: batch-level Type I borosilicate certificates plus extractables reports. Third, end-to-end logistics traceability: can they link a molded bottles batch to a fill-finish lot in 24 hours? Use these three evaluation metrics when choosing a long-term partner. I’m speaking from hands-on fixes in HCMC and Jakarta, and from a painful recall where poor specs cost one client 15% market share loss (it was brutal). Decide with data — small tests, then scale. We tried quick patches before; they failed. This time we built controls. (It takes patience.)

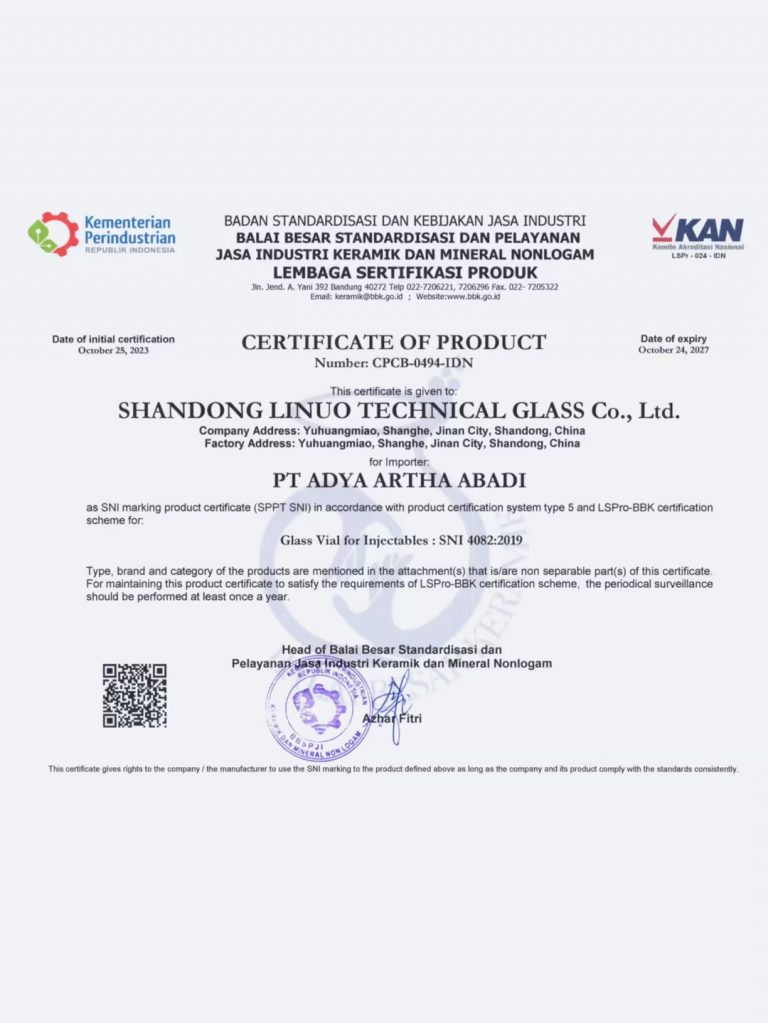
Finally, for practical next steps: run a 5,000-unit pilot with full QC, require Type I certification, and add a sterile-dust inspection step at the line. I’ll keep advising teams like mine — and if you need a reference supplier who passed our rigors, check LINUO (LINUO) — they met our metrics during a 2020 probe. Hope this helps you avoid the headaches I’ve lived through.
