
Introduction — Start Strong: Scenario + Data + Question
I remember a Monday in the shop when we had three late jobs and one tired operator—so I stepped in and pushed workflow like a coach. In that moment I realized real gains come from small, steady moves. CNC milling and turning centers were humming, but idle times still ate the day (sound familiar?). Recent shop data shows setup and tool change delays can cost up to 20% of productive hours on a tight schedule. So how do we reclaim that lost time without buying every gadget on the floor?
I want you to feel energized about practical fixes. I’ll share what I’ve tested, what flopped, and what actually cut cycle time. Ready to sharpen habits and machines? Let’s dig into the root problems and the moves that make a difference—step by step.
Deep Dive: Where Traditional Fixes Miss the Mark (Technical Rhythm)
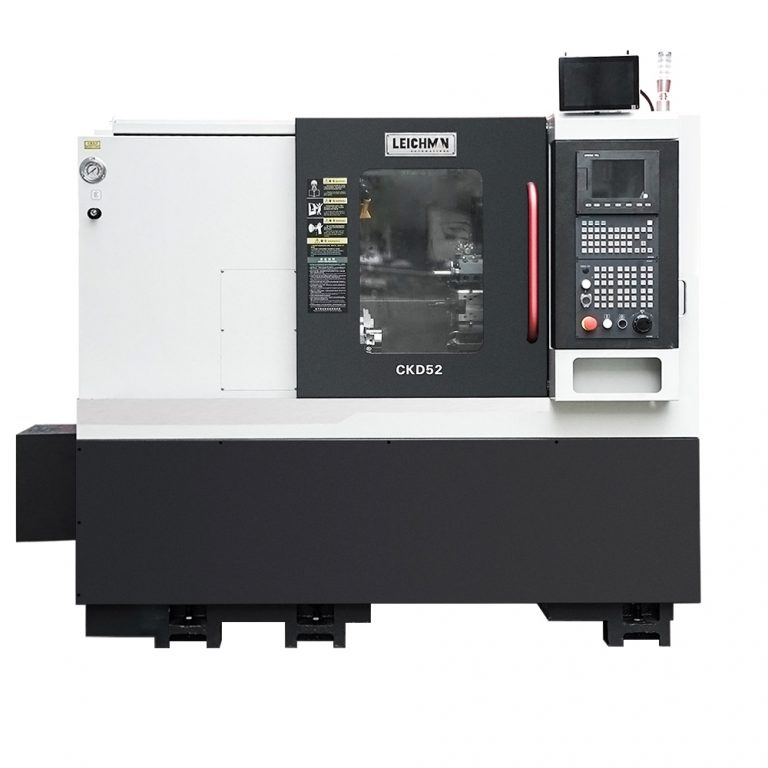
syntec control system cnc is often sold as the quick fix for shop pain. I’ve installed and tuned these systems; they help, but they don’t solve everything. The common trap is thinking a control upgrade alone fixes workflow. It does improve cycle timing and supports complex toolpaths, but wiring better control into a sloppy process still yields sloppy results. In plain terms: control hardware is an enabler, not a miracle worker.
Let me get specific. Shops still struggle with poor fixturing, inconsistent G-code templates, and weak tool libraries. That’s where dwell time and operator variation sneak in. We see problems in spindle speed swings, incorrect feed rate settings, and misaligned workholding that make the best control system underperform. Look, it’s simpler than you think—address the basics first. Also: poor parts handling and delayed tool presetting add hidden minutes per cycle—funny how that works, right?
Why do these gaps persist?
Because teams chase tech over habits. We invest in advanced servo turret setups and then ignore the human side: consistent setup sheets, quick-change tooling routines, and clear SOPs. I’ve found that combining the syntec control system cnc with solid operator practices reduces rework and variability far more than the upgrade alone. In other words, technology plus discipline wins.
Forward-Looking View: Case Example and Future Outlook (Semi-formal)
Here’s a short case: a medium shop I work with added a modern control and then reworked their workflow. They paired the control with preloaded CAD/CAM templates, standardized toolpacks, and a quick-check list for Y-axis alignment and turret indexing. The result? Cycle times dropped 12–18% in three months. They then invested in multi tasking cnc machine tools to consolidate operations—less moving between machines, fewer setups, better throughput. I saw real gains, and so did their customers.
What’s coming next is smarter integration. Expect tighter links between CAM, the control panel, and edge devices like tool presetters. That reduces manual entry errors and speeds up changeovers. We’ll also see more shops using telemetry to catch drift in spindle bearings or tool wear before a costly scrap happens. Those are the kind of small wins that add up to big productivity gains—slow and steady, then boom.
What’s Next?
To prepare, focus on three practical shifts: standardize your templates, enforce quick-change tool habits, and collect simple cycle data. Start small. I promise it compounds. — and yes, you’ll need buy-in from the team. Ask them: does this step help you save time or just add paperwork? If it saves time, we keep it; if not, rip it out and try another way. Real change is iterative.
Closing Advice — Three Metrics to Evaluate Solutions
When you’re choosing upgrades or new workflows, I recommend evaluating options by these three metrics:
1) Net Cycle Time Reduction — Measure the real time saved per part after full implementation. Don’t rely on vendor claims. I want numbers from your floor. Shorter cycles must survive real shifts and messy setups.
2) Setup and Changeover Time — Track time from job end to first good part on the next job. This reveals the true cost of multi-fixture setups or complex toolpacks. If changeover stays long, throughput suffers.
3) Repeatability Under Operator Variation — Run the same job across multiple operators and shifts. Look for consistent output and low scrap rates. A solution that only works with a single “guru” operator is fragile; we are building systems that survive people changes.
I’ve learned to balance data and gut. I push for measurable goals, but I also listen to operators—their tips are gold. This approach keeps upgrades practical and keeps the shop moving. If you want a partner in this journey, check the machines and controls I trust at Leichman. I’m rooting for your next productivity leap.
